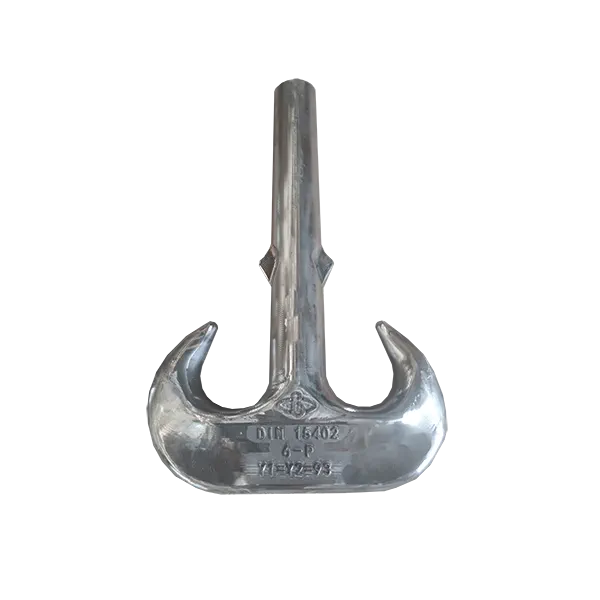
A crane hook is one of the most safety-critical components in any lifting operation. Unlike a cast part that is simply poured and left to cool, a forged hook is worked from red-hot solid steel in a way that preserves and aligns the metal’s grain structure — and that difference is exactly why forged hooks deliver superior strength, fatigue life, and reliability.
This article summarizes the manufacturing and testing process of forged crane hooks — from forging and heat treatment through to the destructive and non-destructive testing a safety-critical hook must pass before it enters service. Heavy-duty forged hooks of this kind are produced in single-piece weights of up to 20,000 kg (44,000 lb) and are typically certified by classification societies such as Lloyd’s Register (LRS), DNV, ABS, and Bureau Veritas (BV).
Why Forging Matters
The key advantage of forging lies in what it does to the steel. During forging, the red-hot (solid, not molten) metal is deformed under high pressure, which preserves and directs the molecular grain structure. The result is a component with:
- Higher safety factors
- Excellent fatigue rating
- Lower maintenance costs
- Longer service life
These properties make forged hooks the standard choice for heavy lifting, offshore rigging, mooring, and other demanding applications.
Part 1: The Manufacturing Process
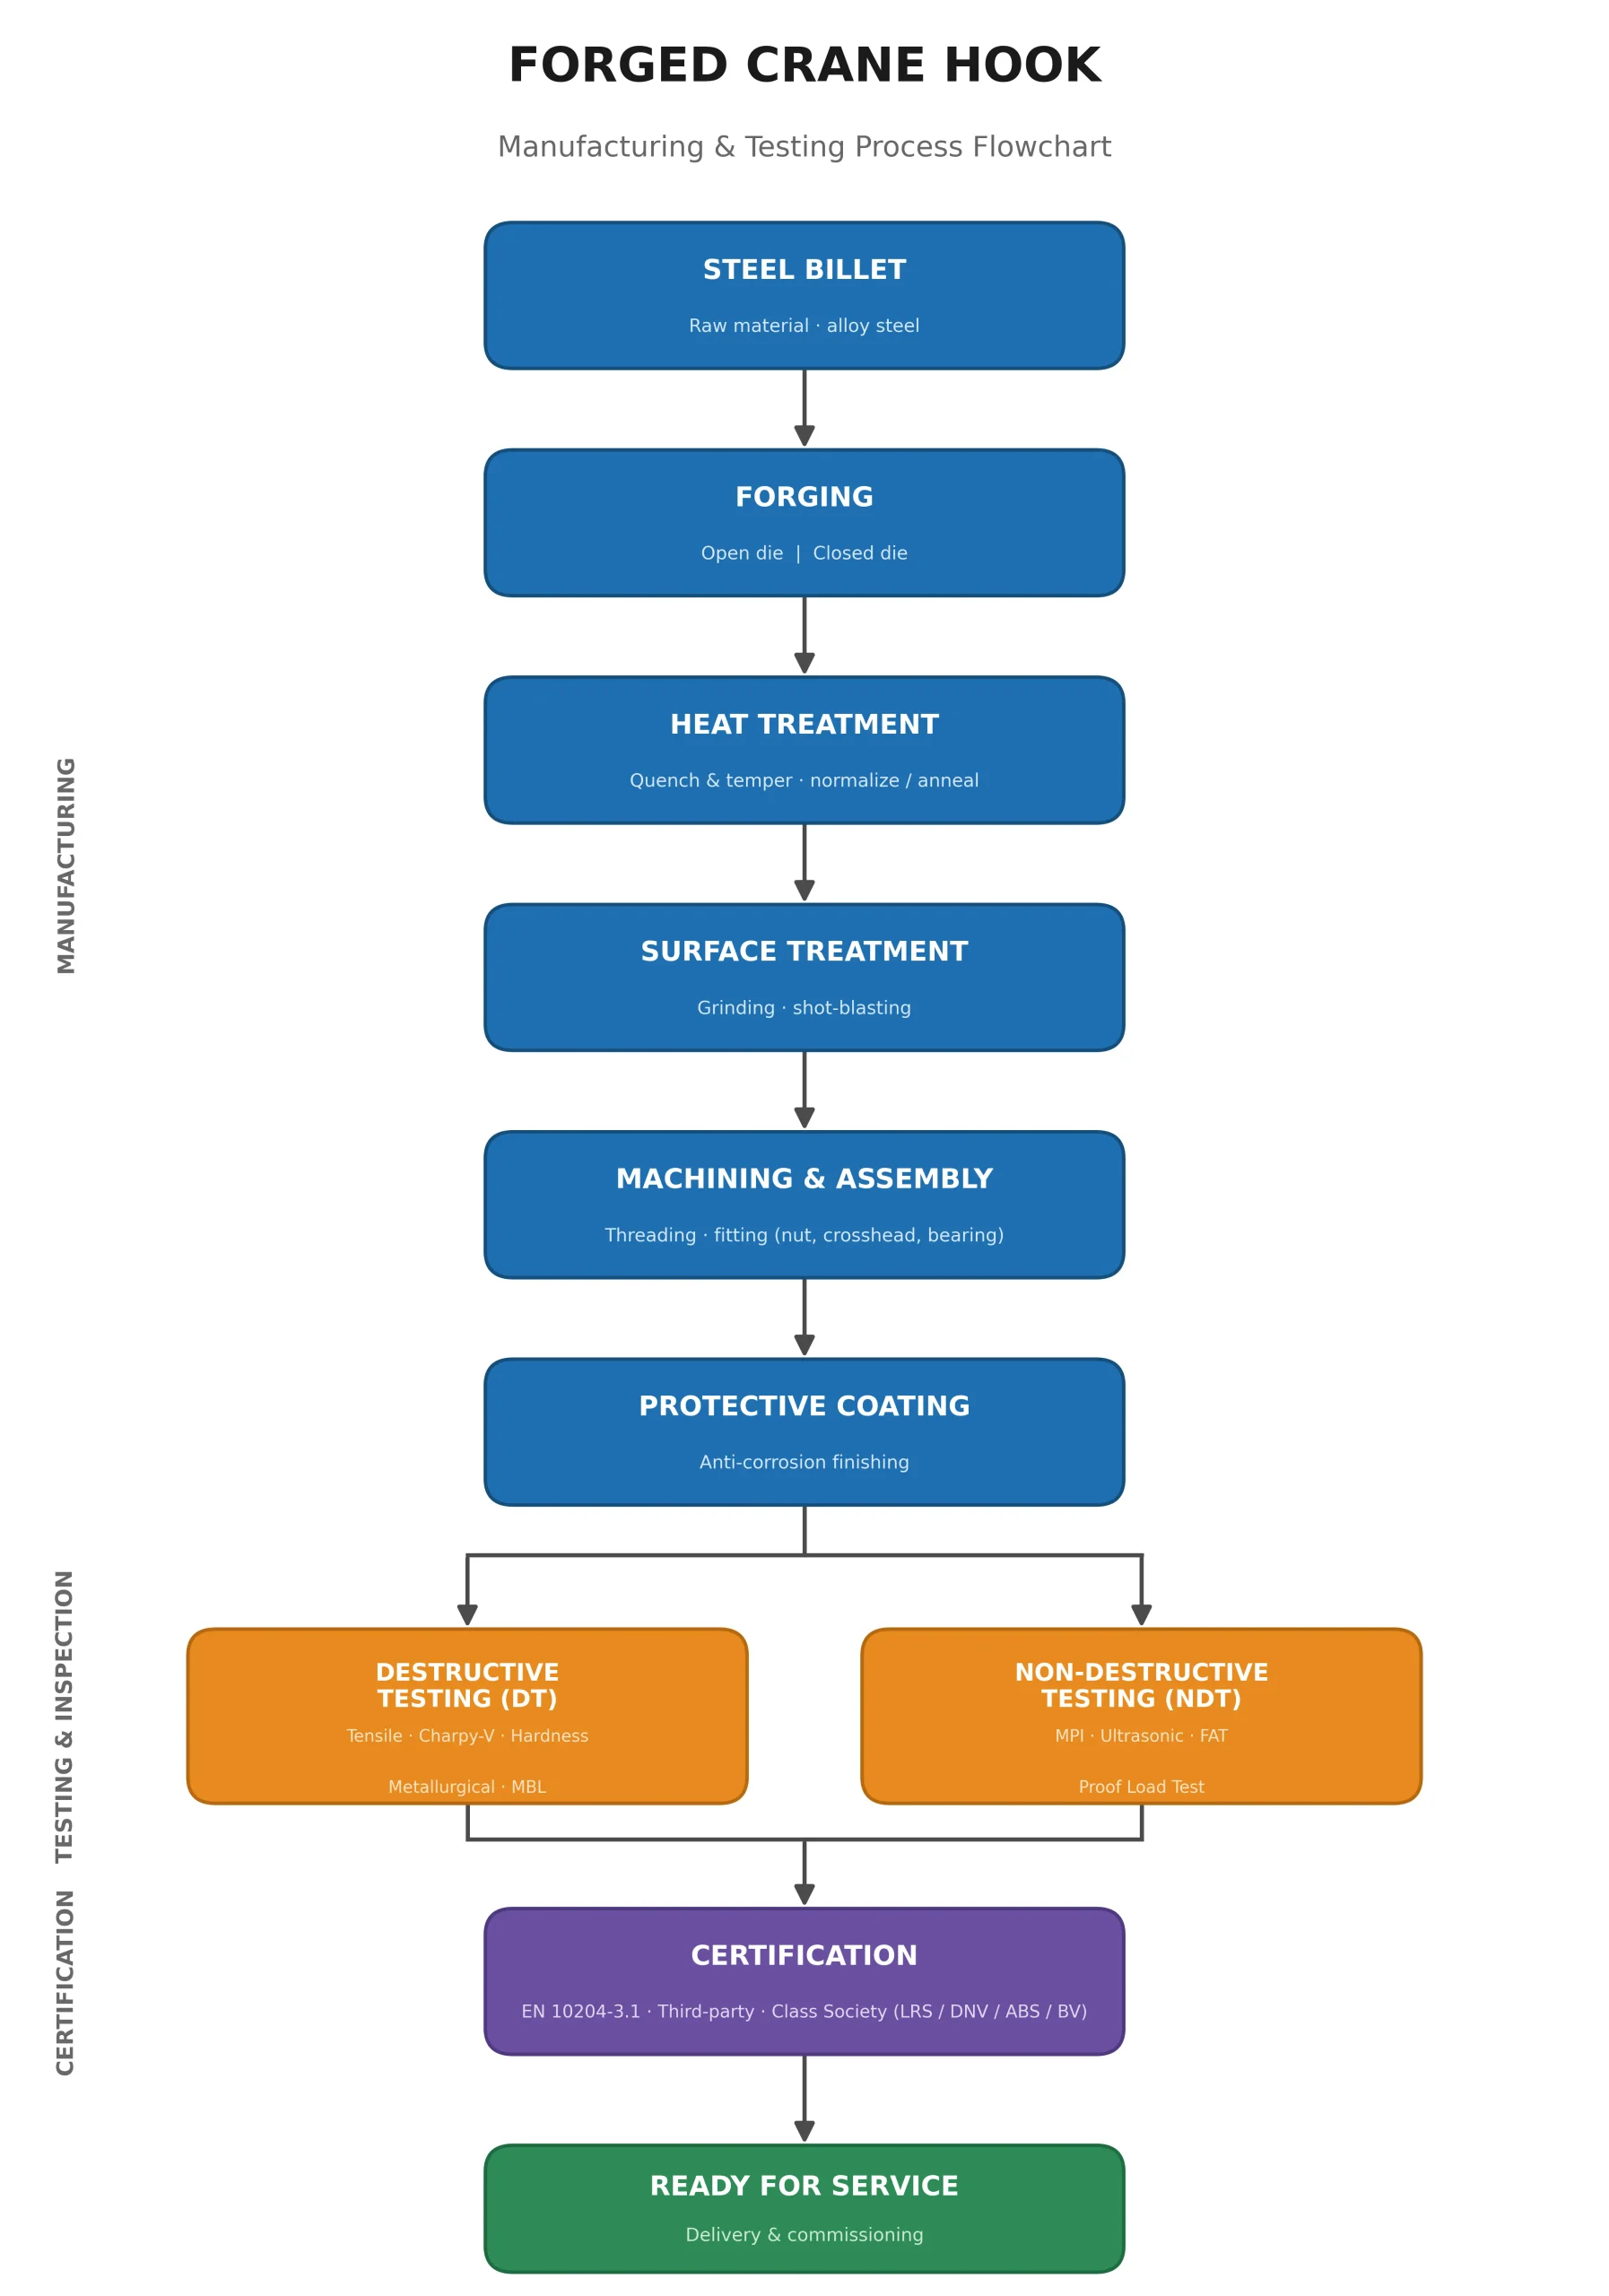
The production of a forged crane hook follows a clear sequence of steps, from raw steel to a finished, installable component.
1. Forging — Open Die vs. Closed Die
The forging method is selected based on the project requirements:
| Method | Characteristics | Best for |
|---|---|---|
| Open die forging | Flexible in shape, more economical | Smaller series, custom/irregular shapes |
| Closed die forging | Less material waste, more economical | Larger series, repeated shapes |
Both methods work the steel in its solid state, preserving the grain flow that gives forged hooks their strength.
2. Heat Treatment
After forging, the hook undergoes heat treatment to achieve optimal physical and mechanical properties:
- Quenching and tempering — to reach the required combination of strength and toughness
- Normalization or annealing — to refine the grain structure and relieve internal stresses
The goal is a carefully balanced set of properties: toughness, strength, and elasticity.
3. Surface Treatment
Once heat-treated, the hook’s surface is processed by grinding and shot-blasting. This step removes any surface defects that could act as stress concentrators and degrade mechanical performance — a critical step for achieving a superior fatigue life.
4. Machining and Assembly
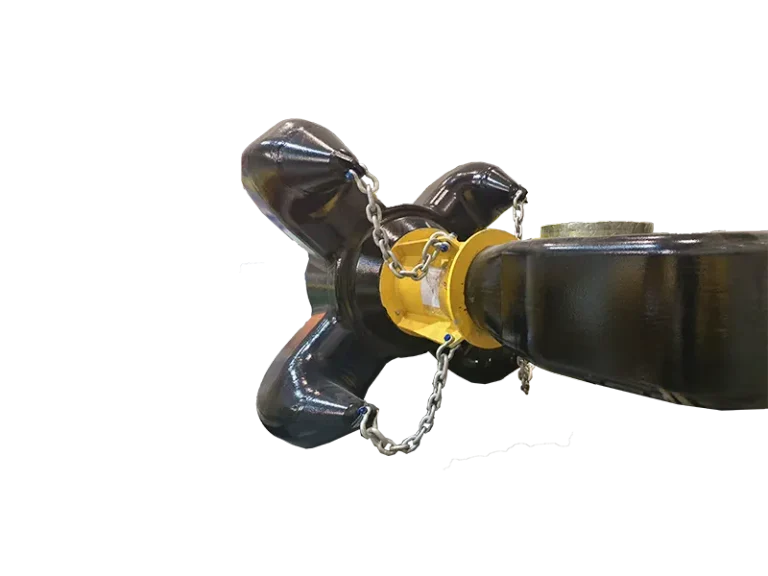
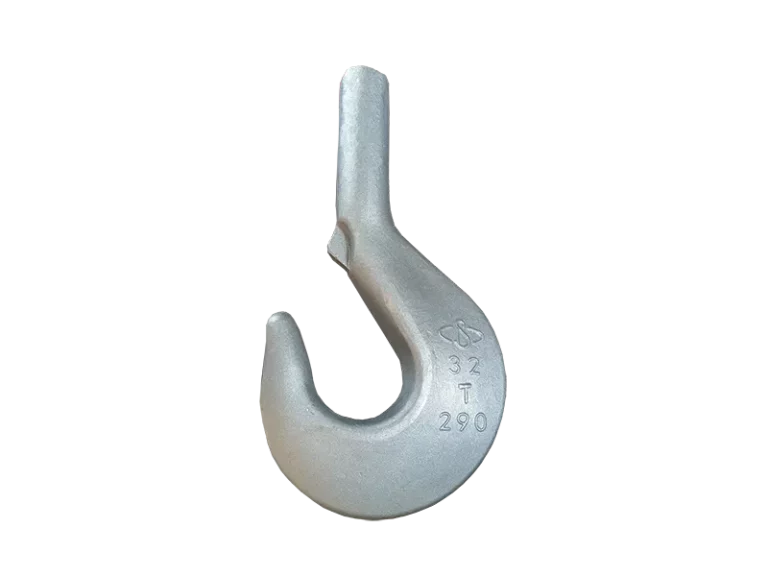
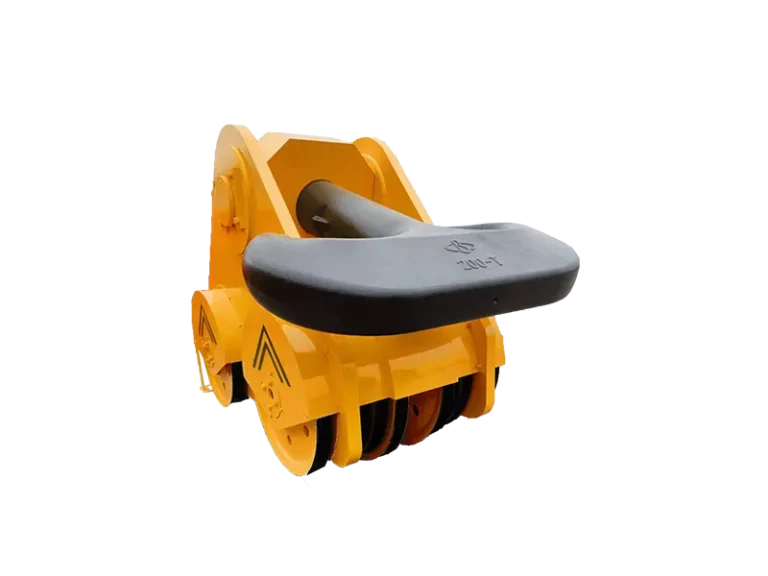
Depending on the customer’s specification, the next step is to machine the component — for example, turning and threading the shank so the hook can be fitted into a hook block. After machining, the individual components are assembled into the complete product (for a ramshorn hook, this typically includes the hook body, nut, crosshead, and thrust bearing).
5. Finishing / Protective Coating
The final manufacturing step is the finish. Specialized coatings are applied to withstand harsh environments, including:
- Extreme weather and temperature
- Chemicals and chlorine
- Salt water and subsea conditions
Manufacturers also typically provide guidance on how to protect the products in these demanding environments.
Part 2: The Testing & Inspection Process
Because a crane hook is a “safety-related” component, it is subjected to high-level testing and inspection both before and during its service life. Testing falls into two broad categories: destructive testing (DT) and non-destructive testing (NDT).
Destructive Testing (DT)
Destructive tests are carried out on sample material to verify the mechanical properties of the steel.
| Test | What it measures |
|---|---|
| Tensile test | Tensile strength, yield point, elongation, and reduction of area — a sample is pulled in controlled tension until failure |
| Charpy-V impact test | The energy absorbed by the material during fracture (high strain-rate test) |
| Hardness test | Surface hardness, measured by applying force with an indenter |
| Metallurgical analysis | Chemical composition, grain size, cavities, and grain-flow orientation |
| Minimum Break Load (MBL) test | The ultimate load at which the component fails |
Non-Destructive Testing (NDT)
NDT verifies the integrity of the finished piece itself, without damaging it. Mandatory NDT methods include:
| Test | What it detects |
|---|---|
| Magnetic Particle Inspection (MPI) | Surface and near-surface discontinuities in ferromagnetic steel |
| Ultrasonic Testing (UT) | Internal imperfections and defects |
| Functional Acceptance Test (FAT) | Correct functional operation of the assembled components |
| Proof Load Test (PLT) | Verification that the hook withstands a specified load without permanent deformation |
The Proof Load Test (PLT) deserves special mention: it is the key acceptance test and is mandatory in some countries (e.g., the USA, and GB/Commonwealth countries) and in specific applications such as offshore, subsea, mooring, and nuclear. Proof load tests are typically carried out on large-capacity test benches (up to several thousand tonnes), oriented vertically or horizontally depending on the product’s size and shape.
Part 3: Certification
Testing is only half the story — the results must be documented and, where required, validated by an independent party.
- EN 10204-3.1 certificate — the mandatory DT and NDT test results form an integral part of the material certificate issued by the manufacturer.
- Third-party validation — tests can be certified by a recognized independent third party.
- Classification society certification — full certification is issued according to the lifting or mooring rules of class societies (LRS, DNV, ABS, BV), based on the scope of supply.
- Guidance and manuals — documentation for correct usage, maintenance, and decommissioning is provided to end users.
Summary
The production of a forged crane hook is a tightly controlled process:
- Forge the steel (open or closed die) to preserve grain structure
- Heat treat (quench & temper, normalize/anneal) for optimal mechanical properties
- Surface treat (grind, shot-blast) to remove defects and improve fatigue life
- Machine and assemble the finished component
- Apply protective coating for the operating environment
This is followed by rigorous verification:
- Destructive tests (tensile, impact, hardness, metallurgical, MBL) confirm material properties
- Non-destructive tests (MPI, UT, FAT, proof load) confirm component integrity
- Certification (EN 10204-3.1, third-party, class society) provides documented proof of compliance
For a safety-critical component like a crane hook, this combination of disciplined manufacturing and exhaustive testing is what separates a reliable forged hook from one that simply “looks the part.”