Note: This document is a comprehensive technical reference compiled from publicly available DIN 15401 Part 1 data and industry sources. DIN standards are copyrighted and available for purchase from Beuth Verlag (www.beuth.de). This reference is intended for technical understanding and quick lookup, not as a substitute for the official standard.
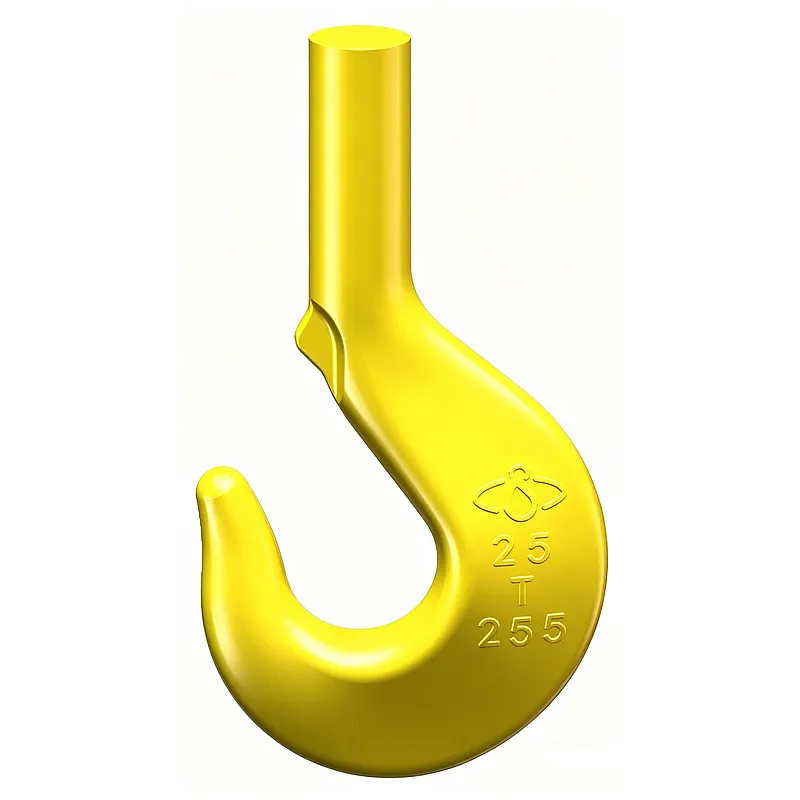
1. Standard Title and Scope
Standard: DIN 15401 Part 1
Full Title (German): Lasthaken für Hebezeuge; Einfachhaken; Rohteile
Full Title (English): Lifting hooks for lifting appliances; Single hooks; Unmachined parts
Scope: DIN 15401 Part 1 specifies the dimensions, materials, forging requirements and marking of unmachined forged single hook blanks (rohlinge) for lifting appliances. These blanks are semi-finished forgings that have completed forging and heat treatment, but have not yet undergone thread cutting, final machining or finishing. They are intended for subsequent machining into finished single hooks per DIN 15401 Part 2.
Applicable hook types: Single hooks with threaded shank, available with nose (RSN) or without nose / flat nose (RFN), in hook numbers ranging from 006 to 250.
Relationship to other standards:
- DIN 15400: Lifting hooks — materials, mechanical properties, lifting capacity and stresses (master standard)
- DIN 15401 Part 2: Single hooks — finished parts with threaded shank
- DIN 15402: Ramshorn (double) hooks — Part 1 unmachined, Part 2 finished
- DIN 15404: Technical delivery conditions for forged lifting hooks
- DIN 15411: Hook suspensions
- DIN 15412: Crossheads
- DIN 15413: Nuts
2. Normative References
The following standards contain provisions which, through reference in this text, constitute provisions of DIN 15401 Part 1:
- DIN 15400: Lifting hooks for lifting appliances — Materials, mechanical properties, lifting capacity and stresses
- DIN 15404: Lifting hooks for lifting appliances — Technical delivery conditions for forged lifting hooks
- DIN EN 10025: Hot rolled products of structural steels
- DIN EN 10083: Quenched and tempered steels
- DIN 50125: Tensile test pieces
- DIN 50115: Charpy impact test
3. Terms and Definitions
- Unmachined part (Rohteil): A forged hook blank that has completed forging and heat treatment, with machining allowance reserved for subsequent thread cutting and final machining. Not ready for lifting service.
- Hook number: A numerical designation (006 to 250) that identifies the hook size and corresponds to the shank diameter d1 and nominal lifting capacity.
- Strength grade: Classification of hook material by mechanical properties (M, P, S, T, V), defined in DIN 15400.
- Shank (Schaft): The straight cylindrical portion of the hook that is threaded in the finished part and connects to the hook block via a nut and crosshead.
- Nose (Nase): The protruding tip at the end of the hook throat, designed to prevent sling disengagement. RSN type hooks have a nose; RFN type hooks have a flat or no nose.
- Throat opening (Maulweite): The clear opening between the hook tip and the hook body, through which slings are loaded.
4. Hook Number Series and Types
DIN 15401 Part 1 defines single hook blanks in the following hook numbers:
006, 010, 012, 020, 025, 04, 05, 08, 1, 1.6, 2.5, 4, 5, 6, 8, 10, 12, 16, 20, 25, 32, 40, 50, 63, 80, 100, 125, 160, 200, 250
Two types are specified:
- RSN: Single hook blank with nose, primarily for smaller hook numbers (006 to 8, with some exceptions).
- RFN: Single hook blank without nose / flat nose, primarily for larger hook numbers (10 to 250, with some exceptions at 05 and 08).
The hook number approximately corresponds to the nominal lifting capacity in tons at a reference strength grade and duty class, as defined in DIN 15400. The actual allowable WLL depends on the strength grade (M/P/S/T/V) and the crane mechanism duty class (M1-M8).
5. Materials and Strength Grades
Per DIN 15400, hook blanks are manufactured in five strength grades from lowest to highest: M, P, S, T and V. The material selection depends on the hook number and strength grade as follows:
| Hook No. Range | Grade M | Grade P | Grade S | Grade T | Grade V |
|---|---|---|---|---|---|
| 006 to 1.6 | StE-285 | StE-355 | StE-420 / 34CrMo4 | 34CrMo4 | 34CrMo4 |
| 2.5 to 40 | StE-285 | StE-355 | StE-420 / 34CrMo4 | 34CrMo4 | 34CrNiMo6 |
| 50 to 250 | StE-355 | StE-420 | StE-500 / 34CrMo4 | 34CrNiMo6 | 34CrNiMo8 |
Material Notes
- Grades M and P: Fine-grained structural steels (StE-285, StE-355, StE-420), normalized condition. Suitable for general and normal-duty lifting applications.
- Grade S: Structural steel (StE-420, StE-500) or low-alloy steel (34CrMo4). For medium-duty applications with higher load requirements.
- Grade T: Quenched and tempered alloy steel (34CrMo4 or 34CrNiMo6). For medium- to heavy-duty cranes requiring higher strength and toughness.
- Grade V: High-strength quenched and tempered alloy steel (34CrMo4, 34CrNiMo6 or 34CrNiMo8). For heavy-duty and critical lifting applications. Note: Grades T and V are not recommended for metallurgical cranes.
- Chinese equivalents: 34CrMo4 ≈ 35CrMo; 34CrNiMo6 ≈ 34Cr2Ni2Mo; 30CrNiMo8 ≈ 30Cr2Ni2Mo; StE-355 ≈ Q345qD; StE-420 ≈ Q420qD.
6. Dimensional Specifications
The following tables provide the complete dimensional specifications for DIN 15401 Part 1 single hook unmachined parts. All dimensions are in millimeters (mm) unless otherwise noted. Weights are in kilograms (kg).
6.1 Main Dimensions — Small Hook Numbers (006 to 8)
| No. | Type | a1 | a2 | a3 | b1 | b2 | d1 | e1 | e2 | e3 | f1 | h1 | h2 | l1 |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 006 | RSN | 25 | 20 | 28 | 13 | 11 | 14 | 60 | 60 | 52 | 14.5 | 17 | 14 | 100 |
| 010 | RSN | 28 | 22 | 32 | 16 | 13 | 16 | 67 | 68 | 60 | 16.5 | 20 | 17 | 109 |
| 012 | RSN | 30 | 24 | 34 | 19 | 15 | 16 | 71 | 73 | 63 | 18 | 22 | 19 | 115 |
| 020 | RSN | 34 | 27 | 39 | 21 | 18 | 20 | 81 | 82 | 70 | 20 | 26 | 22 | 138 |
| 025 | RSN | 36 | 28 | 41 | 22 | 19 | 20 | 85 | 88 | 74 | 22 | 28 | 24 | 144 |
| 04 | RSN | 40 | 32 | 45 | 27 | 22 | 24 | 96 | 100 | 83 | 25 | 34 | 29 | 155 |
| 05 | RFN | 43 | 34 | 48 | 29 | 24 | 24 | 102 | 108 | 89 | 26 | 37 | 31 | 167 |
| 08 | RFN | 48 | 38 | 54 | 35 | 29 | 30 | 115 | 120 | 100 | 29 | 44 | 37 | 186 |
6.2 Main Dimensions — Large Hook Numbers (1 to 250)
| No. | Type | a1 | a2 | a3 | b1 | b2 | d1 | e1 | e2 | e3 | f1 | h1 | h2 | l1 |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 1 | RSN | 50 | 40 | 57 | 38 | 32 | 30 | 120 | 128 | 105 | 31 | 48 | 40 | 197 |
| 1.6 | RSN | 56 | 45 | 64 | 45 | 38 | 36 | 135 | 146 | 118 | 35 | 56 | 48 | 224 |
| 2.5 | RSN | 63 | 50 | 72 | 53 | 45 | 42 | — | — | 132 | 40 | 67 | 58 | 253 |
| 4 | RSN | 71 | 56 | 80 | 63 | 53 | 48 | 172 | 190 | 148 | 45 | 80 | 67 | 285 |
| 5 | RSN | 80 | 63 | 90 | 71 | 60 | 53 | — | — | 165 | 51 | 90 | 75 | 318 |
| 6 | RSN | 90 | 71 | 101 | 80 | 67 | 60 | 218 | 240 | 185 | 57 | 100 | 85 | 380 |
| 8 | RSN | 100 | 80 | 113 | 90 | 75 | 67 | 242 | 268 | 210 | 64 | 112 | 95 | 418 |
| 10 | RFN | 112 | 90 | 127 | 100 | 85 | 75 | 256 | 286 | 221 | — | 125 | 106 | 452 |
| 12 | RFN | 125 | 100 | 143 | 112 | 95 | 85 | 292 | 316 | 252 | — | 140 | 118 | 650 |
| 16 | RFN | 140 | 112 | 160 | 125 | 106 | 95 | 325 | 357 | 280 | — | 160 | 132 | 730 |
| 20 | RFN | 160 | 125 | 180 | 140 | 118 | 106 | 370 | 405 | 330 | — | 180 | 150 | 800 |
| 25 | RFN | 180 | 140 | 202 | 160 | 132 | 118 | 415 | 455 | 360 | — | 200 | 170 | 895 |
| 32 | RFN | 200 | 160 | 225 | 180 | 150 | 132 | 465 | 510 | 400 | — | 224 | 190 | 970 |
| 40 | RFN | 224 | 180 | 252 | 200 | 170 | 150 | 517 | 567 | 447 | — | 250 | 212 | 1041 |
| 50 | RFN | 250 | 200 | 285 | 224 | 190 | 170 | 575 | 635 | 485 | — | 280 | 236 | 1200 |
| 63 | RFN | 280 | 224 | 320 | 250 | 212 | 190 | 655 | 710 | 550 | — | 315 | 265 | 1320 |
| 80 | RFN | 315 | 250 | 358 | 280 | 236 | 212 | 727 | 802 | 598 | — | 355 | 300 | 1470 |
| 100 | RFN | 355 | 280 | 402 | 315 | 265 | 236 | 827 | 902 | 688 | — | 400 | 335 | 1615 |
| 125 | RFN | 400 | 315 | 450 | 355 | 300 | 265 | 920 | 1020 | 750 | — | 450 | 375 | 1790 |
| 160 | RFN | 450 | 355 | 505 | 400 | 335 | 300 | 1035 | 1145 | 825 | — | 500 | 425 | 1990 |
| 200 | RFN | 500 | 400 | 565 | 450 | 375 | 335 | 1150 | 1275 | 900 | — | 560 | 475 | 2248 |
| 250 | RFN | 560 | 450 | 635 | 500 | 425 | 375 | 1280 | 1430 | 980 | — | 630 | 530 | 2505 |
6.3 Radii, Transitions and Additional Dimensions (All Hook Numbers)
| No. | f2 | f3 | g1 | r1 | r2 | r3 | r4 | r5 | r6 | r7 | r8 | r9 |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 006 | — | — | 6.5 | 2 | 3 | 32 | 53 | 53 | 27 | 26 | — | 4 |
| 010 | — | — | 7 | 2 | 3.5 | 35 | 60 | 60 | 31 | 30 | — | 40 |
| 012 | — | — | 7.5 | 2.5 | 4 | 37 | 63 | 63 | 34 | 33 | — | 44 |
| 020 | — | — | 8.5 | 2.5 | 4.5 | 40 | 71 | 71 | 39 | 37 | — | 52 |
| 025 | — | — | 9 | 3 | 5 | 43 | 75 | 75 | 42 | 40 | — | 56 |
| 04 | — | — | 10 | 3.5 | 5.5 | 46 | 85 | 85 | 49 | 45 | — | 68 |
| 05 | — | — | 10.5 | 4 | 6 | 48 | 90 | 90 | 53 | 48 | — | 74 |
| 08 | — | — | 12 | 4.5 | 7 | 52 | 100 | 100 | 61 | 56 | — | 88 |
| 1 | — | — | 12.5 | 5 | 8 | 55 | 106 | 106 | 65 | 60 | — | 96 |
| 1.6 | — | — | 14 | 6 | 9 | 60 | 118 | 118 | 76 | 68 | — | 112 |
| 2.5 | — | — | 16 | 7 | 10 | 65 | 132 | 132 | 90 | 78 | — | 134 |
| 4 | — | — | 16 | 8 | 12 | 71 | 150 | 150 | 103 | 90 | — | 160 |
| 5 | — | — | 18 | 9 | 14 | 80 | 170 | 170 | 114 | 100 | — | 180 |
| 6 | — | — | 18 | 10 | 16 | 90 | 190 | 190 | 131 | 112 | — | 200 |
| 8 | — | — | 23 | 11 | 18 | 100 | 212 | 212 | 146 | 125 | — | 224 |
| 10 | 46 | 26 | 23 | 12 | 20 | 65 | 165 | 236 | 163 | 140 | 12 | 250 |
| 12 | 53 | 34 | 28 | 14 | 22 | 70 | 185 | 265 | 182 | 160 | 16 | 280 |
| 16 | 58 | 35 | 33 | 16 | 25 | 80 | 210 | 300 | 204 | 180 | 16 | 320 |
| 20 | 68 | 45 | 33 | 18 | 28 | 90 | 240 | 335 | 232 | 200 | 20 | 360 |
| 25 | 74 | 45 | 38 | 20 | 32 | 100 | 270 | 375 | 262 | 224 | 20 | 400 |
| 32 | 80 | 45 | 38 | 22 | 36 | 115 | 300 | 425 | 292 | 250 | 20 | 448 |
| 40 | 93 | 55 | 42 | 25 | 40 | 130 | 335 | 475 | 326 | 280 | 25 | 500 |
| 50 | 100 | 55 | 42 | 28 | 45 | 150 | 370 | 530 | 326 | 315 | 25 | 560 |
| 63 | 108 | 60 | 45 | 32 | 50 | 160 | 420 | 600 | 408 | 355 | 25 | 630 |
| 80 | 113 | 60 | 45 | 36 | 56 | 180 | 470 | 670 | 460 | 400 | 25 | 710 |
| 100 | 130 | 70 | 50 | 40 | 63 | 200 | 530 | 750 | 516 | 450 | 30 | 800 |
| 125 | 138 | 70 | 50 | 45 | 71 | 230 | 600 | 850 | 579 | 500 | 30 | 900 |
| 160 | 147 | 70 | 55 | 50 | 80 | 250 | 675 | 950 | 654 | 560 | 30 | 1000 |
| 200 | 154 | 70 | 55 | 56 | 90 | 285 | 750 | 1060 | 729 | 630 | 30 | 1120 |
| 250 | 164 | 70 | 60 | 63 | 100 | 320 | 840 | 1180 | 815 | 710 | 30 | 1260 |
6.4 Approximate Weights
| No. | Weight (kg) | No. | Weight (kg) | No. | Weight (kg) | No. | Weight (kg) |
|---|---|---|---|---|---|---|---|
| 006 | 0.2 | 1 | 3.2 | 10 | 34 | 63 | 600 |
| 010 | 0.3 | 1.6 | 4.5 | 12 | 47 | 80 | 860 |
| 012 | 0.4 | 2.5 | 6.3 | 16 | 66 | 100 | 1220 |
| 020 | 0.6 | 4 | 8.8 | 20 | 112 | 125 | 1740 |
| 025 | 0.8 | 5 | 12.3 | 25 | 160 | 160 | 2480 |
| 04 | 1.1 | 6 | 17.1 | 32 | 220 | 200 | 3420 |
| 05 | 1.6 | 8 | 24 | 40 | 310 | 250 | 4800 |
| 08 | 2.3 | — | — | 50 | 430 | — | — |
7. Dimension Designations Explained
| Symbol | Description |
|---|---|
| a1, a2, a3 | Hook throat and tip dimensions (throat opening related) |
| b1, b2 | Hook body thickness dimensions |
| d1 | Shank diameter (nominal thread diameter for finished part) |
| e1, e2, e3 | Overall width and depth dimensions of hook body |
| f1, f2, f3 | Bearing surface and shoulder dimensions (f2, f3 apply to RFN type large hooks) |
| g1 | Transition radius at shank-hook body junction |
| h1, h2 | Hook depth and throat depth dimensions |
| l1 | Overall length of hook blank (shank + hook body) |
| r1 to r9 | Various fillet and transition radii to reduce stress concentration |
8. Forging Requirements
- Forging process: Hook blanks must be manufactured by closed-die forging (drop forging) or hammer forging (free forging). Cast or welded hooks are not permitted under DIN 15401.
- Metal flow lines: The forging process must produce continuous grain flow lines following the hook contour, eliminating internal metallurgical defects such as porosity, inclusions and laminations.
- Material: Only fine-grained killed steel may be used. The steel must be suitable for forging and subsequent heat treatment.
- Machining allowance: Unmachined parts are supplied with sufficient machining allowance on all surfaces that will be subsequently machined (shank, threads, bearing surfaces, throat opening).
- Surface condition: The forged surface must be smooth and free from harmful defects such as cracks, folds, laps and excessive scale. Local indentations at the shank and curved back junction are permitted within specified tolerances.
- Repair welding: Repair welding of hook forgings is not permitted.
9. Heat Treatment Requirements
- Grades M and P: Normalized condition (normalizing heat treatment) to achieve the required mechanical properties for structural steels (StE-285, StE-355, StE-420).
- Grades S, T and V: Quenched and tempered (Q&T) condition. Quenching forms martensite for high hardness and strength; subsequent high-temperature tempering transforms it into tempered sorbite, achieving the optimal strength-toughness balance.
- Heat treatment before delivery: All unmachined hook blanks must be fully heat-treated before delivery. This eliminates the risk of heat-treatment distortion after final machining.
- Mechanical properties: After heat treatment, the material must meet the minimum yield strength, tensile strength, elongation and impact energy (Charpy V-notch) requirements specified in DIN 15400 for the designated strength grade.
- Hardness: Hardness values after heat treatment must fall within the range specified for the material and strength grade.
10. Surface Treatment and Protection
- Hook blanks must be descaled (rust removal) after forging and heat treatment.
- The surface may be protected with a temporary anti-rust coating (e.g. anti-rust oil or paint) for storage and transportation.
- Final surface treatment (painting, powder coating, etc.) is typically applied after machining, per DIN 15401 Part 2 or customer specification.
11. Marking Requirements
Each unmachined hook blank must be permanently marked with the following information, typically on the shank or a non-critical flat surface:
- Hook number (e.g. 10, 20, 50)
- Strength grade (M, P, S, T or V)
- Manufacturer identification (name or trademark)
- Material specification (where required by customer or applicable standard)
- Heat number / batch number for traceability
Marking must be applied by stamping, die-forging or other permanent method that does not create harmful stress concentrations in load-bearing areas.
12. Inspection and Testing
Per DIN 15404 (technical delivery conditions for forged lifting hooks), the following inspections apply:
- Visual inspection: Full surface examination for cracks, folds, laps and other surface defects.
- Dimensional inspection: Verification of key dimensions against the standard tables, with machining allowance confirmed.
- Magnetic particle testing (MT): For detection of surface and near-surface cracks, particularly at the hook throat, shank transition and hook tip.
- Ultrasonic testing (UT): For detection of internal defects such as inclusions, porosity and laminations, when required by the applicable grade or customer specification.
- Chemical composition verification: Material test certificate (e.g. EN 10204 3.1) confirming chemical composition.
- Mechanical property testing: Tensile test and Charpy impact test on test specimens or test coupons, confirming compliance with the designated strength grade per DIN 15400.
- Hardness testing: Verification of hardness after heat treatment.
Important: DIN 15401 Part 1 unmachined hook blanks are NOT ready for lifting service. They must undergo thread cutting, final machining, proof load testing and final marking per DIN 15401 Part 2 before they can be assembled into a hook block and put into lifting operation. Never use an unmachined blank directly for lifting.
13. Relationship to DIN 15401 Part 2 (Finished Parts)
| Aspect | DIN 15401 Part 1 (Unmachined) | DIN 15401 Part 2 (Finished) |
|---|---|---|
| State | Forged and heat-treated blank | Fully machined, threaded, tested |
| Shank thread | Not cut (machining allowance) | Threaded per specification |
| Bearing surfaces | Not machined | Precision machined |
| Proof load test | Not required (blank stage) | Required (2 x WLL) |
| Ready for service | No | Yes |
| Typical user | Crane OEMs with in-house machining | End users, crane assemblers |
14. Summary
DIN 15401 Part 1 defines the complete technical specification for forged single hook unmachined parts (blanks), covering hook numbers 006 through 250 in two types (RSN with nose, RFN without nose). The standard specifies dimensions in full detail (28 dimensional symbols per hook size), materials across five strength grades (M, P, S, T, V), forging requirements (closed-die or hammer forging only, no casting or welding), heat treatment (normalized for M/P, quenched and tempered for S/T/V), marking, and inspection requirements. These blanks serve as the standard semi-finished forgings from which finished single hooks per DIN 15401 Part 2 are machined.